Choosing the best Sigma Welded Aluminum Joints manufacturers in 2026 requires more than comparing prices or polished product images. Buyers need evidence of process control, alloy knowledge, and repeatable joint performance. A supplier may produce attractive welds yet struggle with porosity, distortion, or inconsistent penetration under production pressure.
Dr. John C. Lippold, a respected welding-metallurgy educator, offers a practical principle: “Aluminum welding demands control of heat, cleanliness, and metallurgy at every stage.” This idea guides our evaluation of Sigma Welded Aluminum Joints manufacturers. We examine their experience with 6061, 6063, and 5083 aluminum alloys, along with their handling of oxide removal, joint fit-up, and thermal distortion. Small details matter. A visible weld bead is not enough.
Reliable manufacturers should provide material certificates, welder qualifications, inspection records, and clear traceability. Certifications such as ISO 3834 or AWS D1.2 can strengthen confidence, but certificates alone do not prove daily consistency. Ask for sample sections, dimensional reports, and evidence of non-destructive testing. When appropriate, tensile testing and macro-etch inspections reveal weaknesses hidden beneath a clean surface.
No ranking is flawless. Supplier capacity can change quickly. Even experienced factories make mistakes. The strongest candidates explain those risks openly and show how corrective actions are managed. This 2026 guide compares technical capability, production reliability, quality documentation, customization support, and long-term service. The goal is not to identify the cheapest source. It is to identify a manufacturer capable of producing stable, safe, and application-ready aluminum joints.
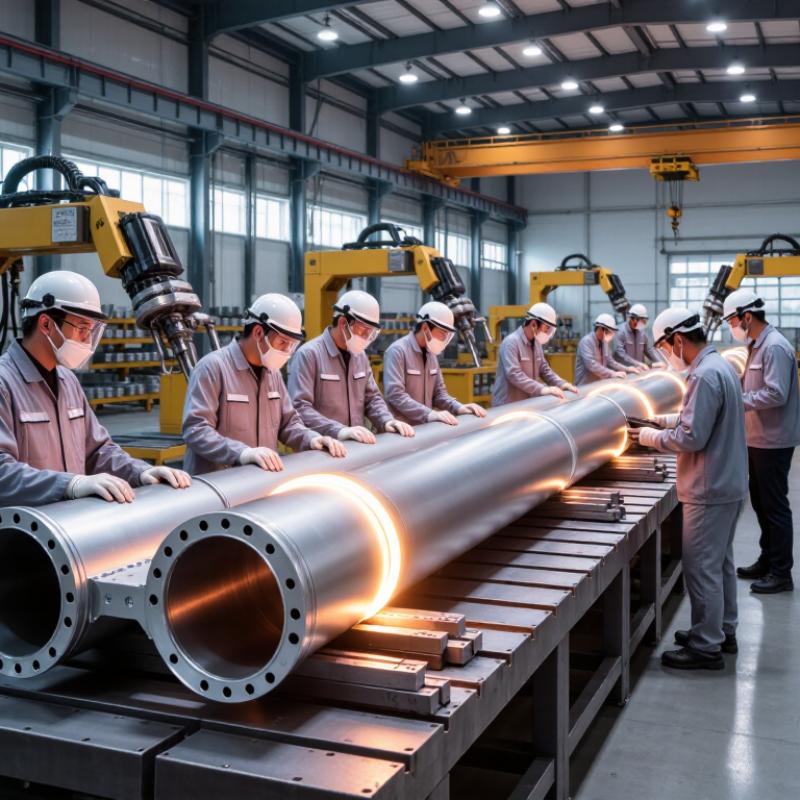
Sigma welded aluminum joints are defined by their geometry, alloy selection, and service purpose. The “sigma” profile may describe a V-like or angled joint that guides load toward the weld zone. Its exact shape should be confirmed by the engineering drawing, not assumed from the name.
Joint geometry controls access, penetration, and stress concentration. A narrow root can restrict fusion, while an oversized gap increases distortion. Common aluminum alloys include 5xxx grades for corrosion resistance and 6xxx grades for formed structural parts. Each alloy responds differently to heat. Weld discoloration alone cannot prove joint quality.
Practical fabricators inspect fit-up, cleaning, shielding gas flow, and interpass temperature. They also examine the finished joint for porosity, undercut, cracks, and incomplete fusion. Marine frames, vehicle structures, heat-exchanger supports, and lightweight enclosures may use these joints when weight reduction matters. The design still needs load calculations and suitable inspection criteria. A strong-looking bead can hide weak internal bonding.
Tips: Confirm the joint profile before production. Remove oxide layers carefully. Keep filler metal compatible with the base alloy. Record welding parameters for repeatability. Measure twice.
One detail deserves reflection: “Sigma” is not always a universal technical term. Different workshops may use it differently. A reliable manufacturer should clarify the geometry, alloy temper, welding process, tolerance, and inspection method before quoting. That conversation often prevents expensive rework.
Sigma welding is commonly associated with gas metal arc welding (GMAW/MIG). For an equal-leg fillet weld, the ideal effective throat is 0.707 times the weld-leg length. The chart shows the resulting geometric throat used for preliminary joint sizing.
Aluminum 5xxx alloys such as 5052 and 5083 are non-heat-treatable and are widely used for sheet, tanks, marine structures, and corrosion-resistant fabrications. 6xxx alloys such as 6061 and 6063 are heat-treatable and common in frames, extrusions, and transportation structures, although welding can soften the heat-affected zone. Many 7xxx alloys have limited fusion-weldability and require specific alloy and procedure qualification. Final weld dimensions must comply with the applicable design code and account for load, joint access, porosity, distortion, filler selection, and heat-affected-zone strength.
For 2026, sigma welded aluminum joints should be judged by measured tensile data, not bead appearance. The often-cited 6061-T6 tensile strength is about 310 MPa for unwelded base material. The Aluminum Association and ASM Handbook both explain that welding can soften the heat-affected zone. Therefore, a welded joint may not retain the full temper strength.
The practical target is different. Published studies commonly report approximately 200–240 MPa ultimate tensile strength for properly welded 6061-T6 joints, depending on process, filler, thickness, and heat input. AWS D1.2/D1.2M recommends procedure qualification, visual inspection, and mechanical testing for structural aluminum welds. A manufacturer should provide actual test certificates, fracture locations, and batch traceability. Numbers without test conditions are weak evidence.
Watch the details. A clean 6-millimeter joint can still fail beside the weld. Excessive heat enlarges the softened zone, while poor shielding leaves small pores. In shop audits, even minor surface contamination has changed results. That is easy to overlook. Joint design also matters, especially throat size and load direction. The 310 MPa figure remains useful as a benchmark, but it should not be presented as the guaranteed strength of every welded joint. More testing is still needed.
Selecting a 2026 welded aluminum joint manufacturer requires more than attractive samples. Global primary aluminum production reached about 70 million metric tonnes in 2023, according to the International Aluminium Institute. That scale increases the need for disciplined welding controls. AWS D1.2 should define joint design, workmanship, inspection, and acceptance requirements. ISO 9606-2 verifies that each welder can produce qualified aluminum welds within approved ranges. Experience matters here. A certificate cannot replace stable hands and clean preparation.
Look for traceable material certificates, controlled filler-wire storage, and calibrated welding equipment. Fit-up still matters. Inspectors should record alloy, thickness, joint type, shielding gas, and welding parameters before production. Visual inspection should check porosity, undercut, cracks, and incomplete fusion. Critical assemblies may require radiographic or ultrasonic testing, depending on the design and contract. These details expose weak process control early.
ISO 9001 adds the management structure behind technical work. The ISO Survey 2022 reported more than 1.2 million ISO 9001 certificates worldwide, showing how widely quality systems are used. However, certification alone proves little without useful records and corrective action.
Audits should sample real job travelers, welder qualifications, nonconformance reports, and final inspection data. Records tell the truth. No system is flawless. Even experienced manufacturers can miss contamination or inconsistent torch angles, so independent inspection and periodic procedure reviews remain necessary.
2026 Best Sigma Welded Aluminum Joints Manufacturers?
Choosing a reliable manufacturer requires more than attractive samples. Inspect weld cross-sections for porosity, lack of fusion, and trapped contamination. Qualified suppliers should report pore size, location, and acceptance criteria. Ask for radiographic or computed tomography results when joint failure carries serious consequences. Visual inspection alone misses internal defects.
Distortion deserves equal attention. Request dimensional reports before and after welding, using calibrated gauges or coordinate measuring equipment. Review fixture design, heat input, sequence control, and correction records. For fatigue-critical joints, require cyclic test results with load levels, stress ratios, and failure locations. A credible manufacturer connects every result to material certificates, weld operator identification, machine settings, and production dates. Traceability should reach the individual joint, not only the shipment.
Tips: Audit a recent production batch, not only a polished sample. Compare reported porosity with independent inspection. Check whether fatigue data reflects your thickness and loading pattern. Ask difficult questions. Some records may look complete but remain too vague for confident decisions. No screening method is perfect, and supplier data can contain gaps. Record those gaps before approval.
Anonymous manufacturer-screening matrix for welded aluminum joint suppliers. Values are engineering acceptance targets and representative qualification ranges based on commonly used aluminum welding procedures and applicable ISO, AWS, ASTM, and EN practices.
| Supplier Category | Typical Aluminum Joint Scope | Porosity Acceptance | Distortion Control | Fatigue Qualification | Traceability Evidence | Process Controls | Screening Status | Risk Level |
|---|---|---|---|---|---|---|---|---|
| High-volume robotic fabricator | 5083, 5754, 6061, and 6082 aluminum assemblies; MIG/GMAW and robotic pulse welding; medium-to-large batch production. | <2% volumetric pore indication in radiographic sample areas; no clustered or interconnected porosity permitted in primary load paths. | Typical angular distortion controlled to ≤1.5°; dimensional capability commonly maintained at ±1.0–2.0 mm, depending on assembly size. | Procedure qualification normally supported by cyclic testing or design allowables; suitable target is ≥1 million cycles at the specified design stress range. | Weld ID, operator ID, wire-lot record, shielding-gas batch, parameter log, inspection result, and nonconformance history linked to a serial or batch number. | Closed-loop wire feed, gas-flow monitoring, programmed heat input, fixture validation, and first-off dimensional inspection. | Strong candidate | Low |
| Certified structural aluminum specialist | Load-bearing frames, transport structures, marine components, and structural profiles using 5083, 6061, and 6082 alloys. | Radiographic or ultrasonic inspection defined by contract class; rejectable indications controlled according to the applicable weld quality level and joint category. | Typical profile or frame straightness target of ≤2 mm per metre after welding, with calibrated fixtures and controlled weld sequencing. | Fatigue assessment generally based on weld-detail classification, stress-range design, and representative coupon or component testing; target evidence should cover the intended load spectrum. | Full WPS/PQR package, welder qualification, material certificates to EN 10204 3.1 or equivalent, filler-metal certificates, and inspection release records. | Qualified welding coordinators, preheat/interpass monitoring where applicable, controlled cleaning, and documented repair procedures. | Strong candidate | Low |
| Precision TIG fabrication shop | Thin-wall 5052, 6061, and 6063 components; visible cosmetic joints; low-to-medium production volumes. | Visual inspection and dye penetrant testing are common; acceptance typically requires no cracks, lack of fusion, or surface-connected linear indications. | Typical dimensional tolerance of ±0.5–1.5 mm for small assemblies when dedicated fixtures and balanced weld sequences are used. | Fatigue data may be limited to procedure-level evidence; project-specific testing is recommended for highly cycled or safety-critical joints. | Usually provides heat-number traceability, operator records, inspection reports, and drawing revision control; digital parameter capture may be limited. | Manual torch control, controlled tungsten preparation, joint-cleaning procedures, fixture checks, and visual weld-profile standards. | Acceptable with verification | Medium |
| Hybrid laser-MIG fabricator | Thin-to-medium aluminum sheet and extrusion assemblies requiring low heat input, high throughput, and limited weld distortion. | Process capability can achieve low pore occurrence when surface preparation and shielding are stable; acceptance should be confirmed through macrosections and radiography. | Typical distortion target of ≤0.8° on suitable thin-section geometries; performance is highly dependent on fit-up and joint gap control. | Potentially favorable fatigue performance because of reduced heat input, but laser transition zones and lack of fusion must be specifically qualified. | Strong digital records are possible, including laser power, travel speed, wire feed, gas flow, alarm history, and component genealogy. | Automated seam tracking, machine-vision inspection, controlled focal position, gap monitoring, and parameter lockout. | Strong candidate | Low to medium |
| Large-format manual fabrication plant | Oversized frames, tanks, platforms, and custom aluminum structures; predominantly manual MIG/GMAW welding. | Acceptance varies significantly by welder and joint position; require defined volumetric inspection sampling and documented repair limits. | Typical post-weld correction may be required; dimensional capability commonly ranges from ±2–5 mm for large structures. | Component-level fatigue evidence is often project-specific; design review should include weld toe geometry, residual stress, and stress concentration effects. | Paper-based or spreadsheet records may include material certificates and welder IDs, but consumable and parameter genealogy can be incomplete. | Manual gas-flow checks, fixture inspection, weld-sequence instructions, hold points, and independent final dimensional inspection. | Acceptable with controls | Medium |
| Prototype and low-volume job shop | Complex one-off brackets, enclosures, development parts, and mixed-alloy assemblies with frequent design changes. | Inspection is commonly visual plus targeted dye penetrant or radiography; acceptance criteria must be written for each drawing and load case. | Results depend on geometry and operator practice; a typical planning allowance is ±2–4 mm before final machining or straightening. | Fatigue qualification is usually unavailable unless separately commissioned; not suitable for critical cyclic loads without additional validation. | Basic batch traceability may exist, but complete linkage between material heat, filler wire, settings, inspection, and repair history requires audit confirmation. | WPS availability, calibrated measuring equipment, documented cleaning, and controlled revision management should be verified before approval. | Conditional | Medium to high |
| Post-machined welded assembly supplier | Near-net welded blanks for precision machining; aluminum housings, manifolds, structural nodes, and close-tolerance assemblies. | Internal voids must be controlled before machining; CT, radiography, or sectional macrograph evidence may be required for pressure or fatigue-critical parts. | Pre-machining distortion target commonly specified at ≤1–2 mm over the functional datum span, subject to stress-relief strategy. | Fatigue suitability depends on weld location relative to machined features; require component-level validation where welds remain in the load path. | Typically capable of linking weld batch, machining route, coordinate inspection, heat treatment, repair, and final inspection to a serialized unit. | Datum-based fixtures, machining allowance control, coordinate-measuring inspection, heat-treatment records, and controlled weld repairs. | Strong candidate | Low to medium |
| General metalwork supplier without dedicated aluminum system | Mixed-material fabrication with occasional aluminum work and limited dedicated aluminum welding equipment. | Porosity, oxide inclusions, and lack of fusion risk may be elevated if cleaning, torch setup, liner condition, and shielding are not aluminum-specific. | Dimensional capability is inconsistent; distortion correction may rely on manual rework rather than a validated process plan. | Fatigue data is generally unavailable; supplier should not be accepted for safety-critical cyclic structures without independent qualification. | Traceability may stop at the purchase order or material certificate and may not include wire lot, gas, operator, or parameter records. | Verify dedicated aluminum equipment, cleaning tools, gas-flow measurement, calibrated instruments, qualified procedures, and inspection competence. | High verification required | High |
A serious supplier comparison should begin with usable capacity, not advertised capacity.
Ask for monthly Sigma-joint output, active welding cells, shift patterns, and fixture availability. The International Aluminium Institute reported global primary aluminum production above 72 million tonnes in 2024. Material supply is broad, but certified welding capacity remains uneven. A factory may accept 20 tonnes monthly and still lack qualified operators for complex joint geometry.
Testing separates a capable supplier from a convenient one.
Require welding procedure qualifications, operator records, dimensional reports, and traceability from billet to finished joint. ISO 10042 provides quality levels for aluminum fusion weld imperfections. Visual inspection should follow ISO 17637, while radiography or penetrant testing should match joint thickness and risk.
Lead time should include tooling, first-article approval, production, and rework.
The 2024 Logistics Managers’ Index continued to report volatility in transportation and inventory conditions, so a fixed promise may hide risk. Cost comparisons should separate aluminum, filler wire, machining, inspection, packaging, and freight. World Bank commodity data also shows aluminum pricing remains sensitive to energy and supply changes.
I would request three quotations using identical drawings and annual volumes. A spreadsheet can still lie.
Its geometry, alloy, and service purpose define the joint. The profile may be V-shaped or angled. Confirm the exact shape from engineering drawings.
Geometry affects weld access, penetration, distortion, and stress concentration. A narrow root may block fusion. A large gap can create excessive deformation.
5xxx alloys often support corrosion-resistant applications. 6xxx alloys commonly suit formed structural parts. Each alloy reacts differently to welding heat.
No. Discoloration alone cannot confirm a sound joint. Inspect for porosity, cracks, undercut, and incomplete fusion. A strong-looking bead may hide weak internal bonding.
Confirm the joint profile, fit-up, oxide removal, shielding gas, and interpass temperature. Use compatible filler metal. Record welding parameters for repeatable production.
Request cross-section inspections for porosity, contamination, and lack of fusion. Radiographic or computed tomography results may help with critical joints. Visual inspection misses hidden defects.
Request dimensional reports before and after welding. Use calibrated gauges or coordinate measuring equipment. Review fixtures, heat input, welding sequence, and correction records.
Request cyclic test results showing loads, stress ratios, and failure locations. Records should identify materials, operators, machine settings, and production dates. Traceability should reach each individual joint. Some records may still be incomplete.
This guide explains how Sigma Welded Aluminum Joints are designed, produced, and evaluated for demanding structural applications. It covers joint geometry, alloy selection, and common uses, with particular attention to 6061-T6 aluminum, which can deliver approximately 310 MPa tensile strength when properly welded and controlled. The discussion also highlights how welding parameters, heat input, filler selection, and joint preparation affect strength, distortion, and long-term fatigue performance.
For 2026 supplier selection, manufacturers should be assessed through documented quality systems and measurable production data. Important benchmarks include AWS D1.2, ISO 9606-2, and ISO 9001 compliance, along with evidence of porosity control, dimensional accuracy, fatigue testing, material traceability, and weld inspection. A practical comparison should also consider production capacity, testing resources, lead times, customization ability, and total cost. Together, these factors help buyers identify reliable suppliers capable of delivering consistent, durable, and traceable aluminum welded assemblies.